Typical Steels for Induction Hardening
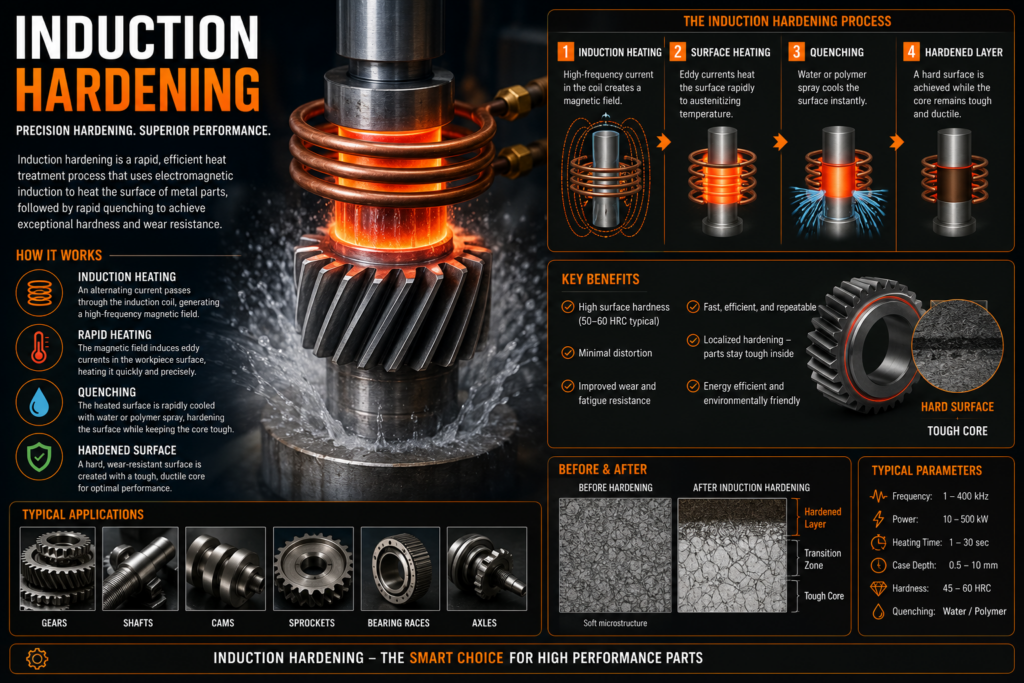
The principles for selecting steel for induction hardening are similar to those used for other hardening methods, but they are not exactly the same. The hardenability of ordinary carbon steel increases as the carbon content rises. For example, steel containing 0.2% carbon, such as 1020 steel, can usually be hardened only to about HRC 48, while steel containing 0.45% carbon, such as 1045 steel, can be hardened to about HRC 60.
Adding alloying elements such as chromium, nickel, molybdenum, and tungsten can improve hardenability by shifting the nose of the S-curve to the right. In through hardening, ordinary carbon steel requires a very fast cooling or quenching rate to avoid the nose of the S-curve and prevent softening. Because heat conduction is slow, the inner layer beneath the hardened surface may cool more slowly and undergo incomplete martensitic transformation, which can cause softening.
Even during surface hardening, heat conducted from the center of the workpiece to the surface can slow the surface cooling rate. This may produce an effect similar to forming a soft pearlitic surface. If a quenchant more severe than oil is used, excessive deformation may occur. Therefore, by adding a small amount of alloying elements, oil quenching can be used to minimize deformation while still achieving the required hardness.
Another reason for adding alloying elements is to improve the mechanical strength of steel, including tensile strength, yield strength, impact resistance, and fatigue performance.
Surface induction heating has a strong influence on steel selection. Since only the surface layer is heated, incomplete transformation below the surface layer is generally not a problem. Rapid surface heating can also be used for fast quenching without creating serious deformation from internal stress. Because the center of the workpiece is neither heated nor quenched, it retains its original strength. These two effects show that ordinary carbon steel can often replace more expensive alloy steel that would otherwise be required for hardening by other heating methods.
Another reason ordinary carbon steels are suitable for induction heating is that they dissolve into solid solution quickly and at lower temperatures than alloy steels. This allows shorter heating times, reduces heat loss to the center of the workpiece, and improves production efficiency. Water quenching can also be used, which is more economical than oil quenching. However, when the center of the hardened workpiece must have high strength, alloy steel is still required.
For induction surface hardening, suitable carbon and alloy element ranges include:
- C = 0.35-0.60%
- C = 0.30-0.40%, Mn = 0.60-1.90%
- C = 0.30-0.45%, Ni = 3.00-5.00%
- C = 0.35-0.45%, Ni = 0.46-0.70%, Cr = 0.30-0.60%
- C = 0.35-0.45%, Ni = 1.50-3.50%, Mo = 0.25%
- C = 0.35-0.45%, Cr = 1.00%, Mn = 0.60-1.20%
The above examples correspond to SAE steels such as 1040, 1050, 1340, 2345, 3140, and 4640.
Preliminary heat treatment of steel is very important. Most induction heating processes have short heating times, which are not sufficient to homogenize steel with coarse or uneven grains. After heat treatment, free ferrite may remain and cause soft spots. Therefore, annealing, spheroidizing annealing, and similar preliminary heat treatments should be avoided whenever possible.
The ideal preliminary heat treatment is normalizing, because it produces a uniform and well-distributed pearlitic structure. Annealing before induction hardening can produce a deeper hardened layer, but the surface hardness is lower, about HRC 52. Normalizing before induction hardening can produce medium hardness, about HRC 53. Quenching and tempering before induction hardening can produce a thinner hardened layer, about 0.75 mm, but with higher hardness, around HRC 62. In practice, normalizing before induction hardening usually provides a good metallographic structure with a relatively deep hardened layer.
Some steels require a short holding period between the end of heating and the start of quenching, so that carbon can fully dissolve. To eliminate this delay, other induction hardening steels have been developed, including SAE 1000 and 1300 series steels.